
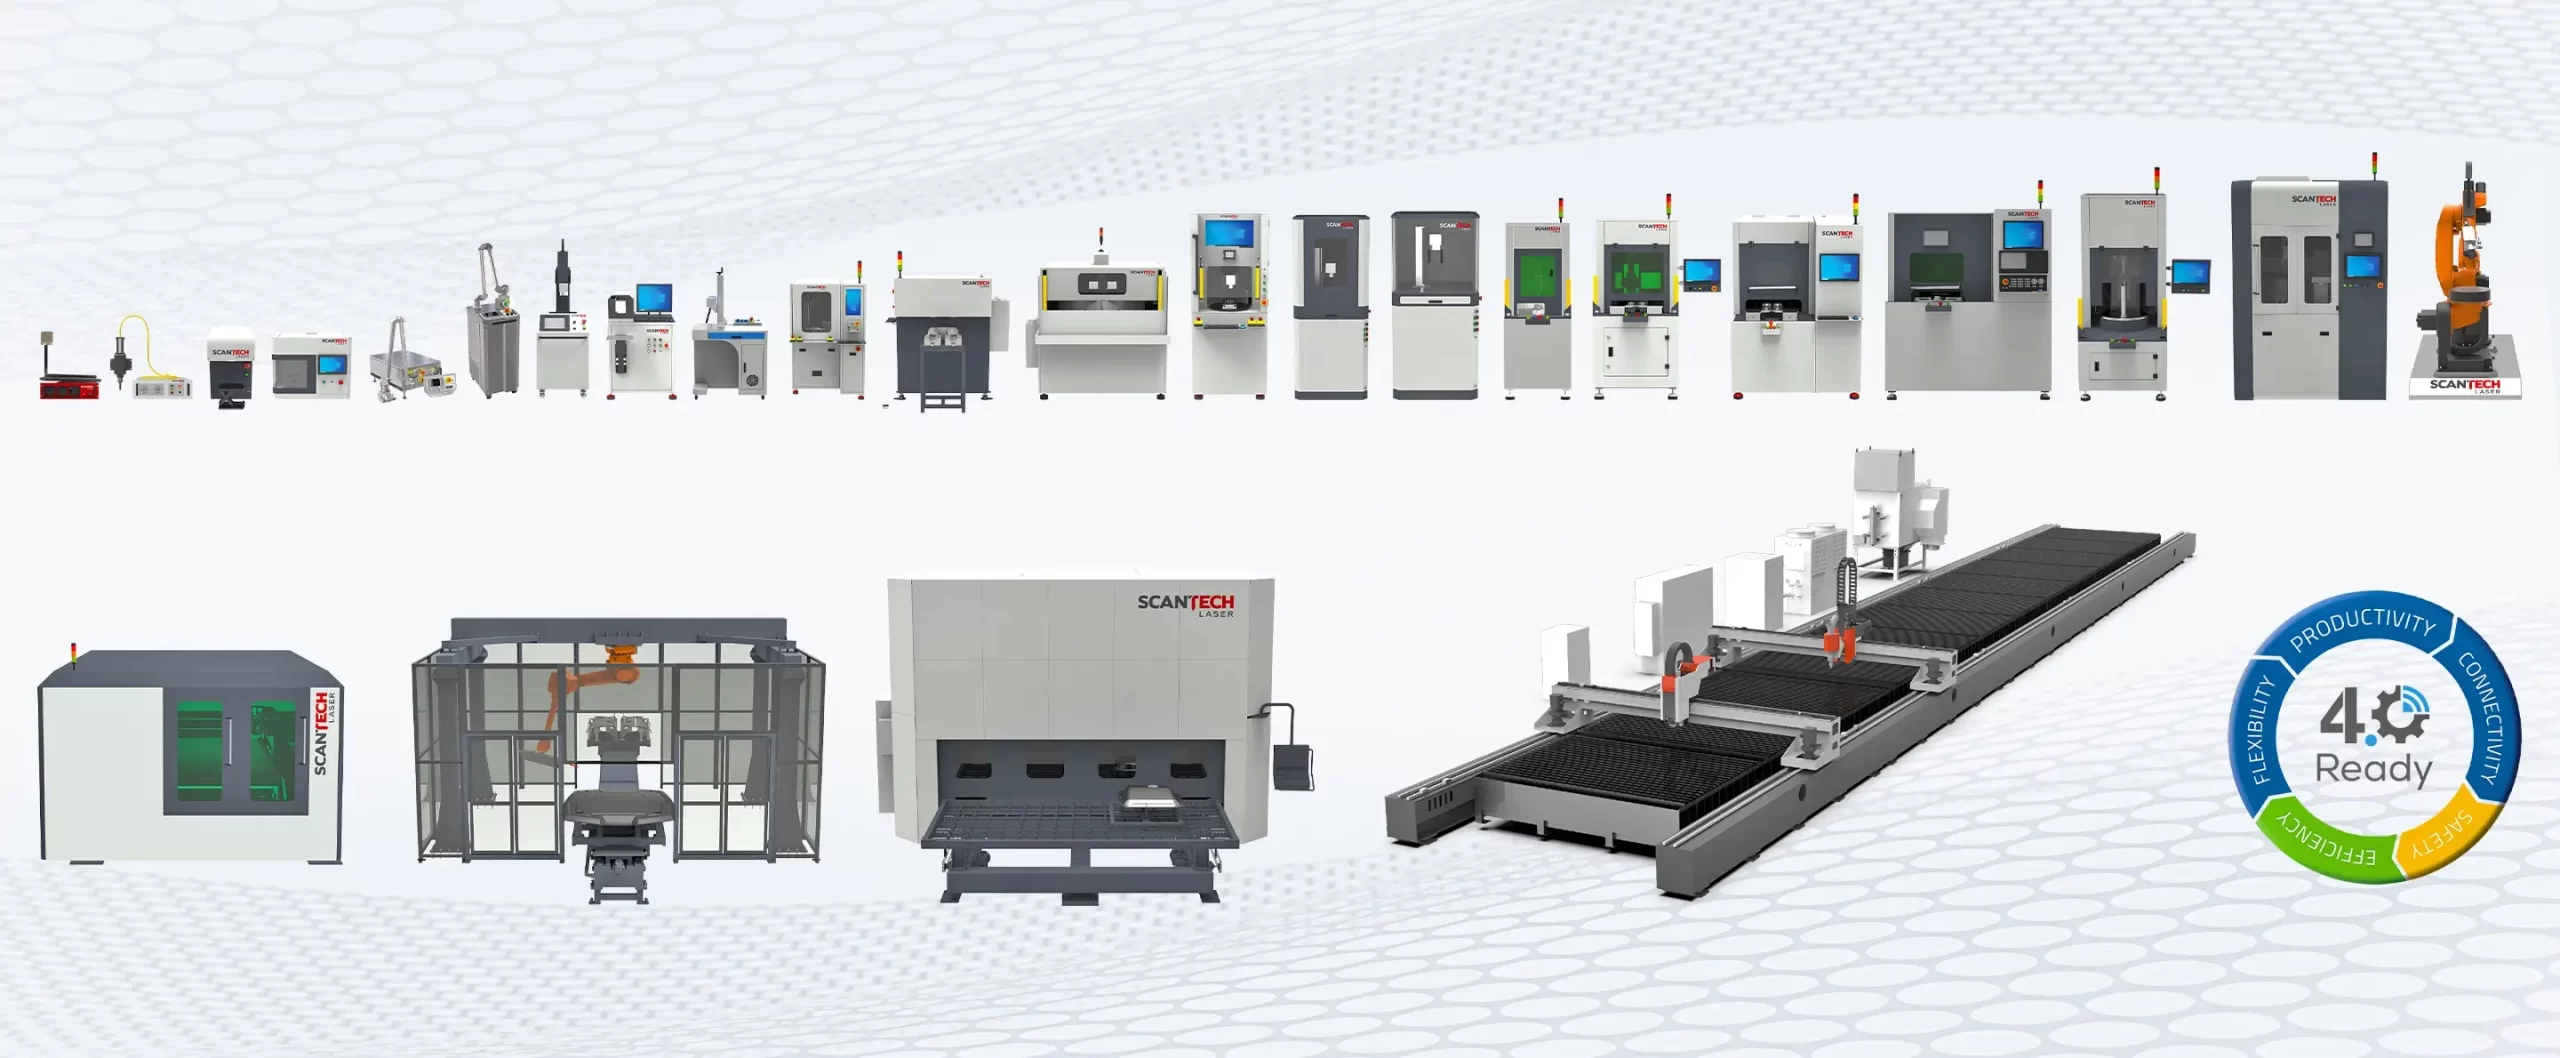
Industrial Laser Hardening Machine
Selective Heat Treatment With Zero Thermal Distortion
Scantech Laser’s industrial laser hardening systems provide non-contact, localized surface transformation for carbon steels, alloy steels, and ductile cast irons. By coupling direct diode or fiber laser sources with real-time closed-loop pyrometry, our systems deliver repeatable case depth and uniform hardness without liquid quenching or mechanical warping.
Localized Hardening
Target specific wear zones such as gear teeth flanks, bearing seats, and punch edges without thermal load on adjacent unhardened areas.
Self-Quenching Process
Rapid thermal conduction into the cold bulk metal eliminates oil or water quenching, removing post-treatment washing and chemical disposal costs.
Closed-Loop Control
Coaxial high-speed infrared pyrometers adjust laser power 1,000 times per second to prevent surface melting and maintain uniform martensite structure.
Laser Hardening vs. Traditional Heat Treatment
Engineered for high-duty automotive, die manufacturing, and heavy machinery parts, laser heat treatment outperforms conventional flame, induction, and furnace carburizing methods across key performance metrics.
| Performance Feature | Laser Hardening (Scantech) | Induction Hardening | Carburizing / Nitriding |
|---|---|---|---|
| Thermal Distortion | Negligible (<0.02 mm); zero post-grinding required | Moderate to High; post-process grinding required | High distortion due to full-body furnace heating |
| Process Speed & Cycle Time | High speed (up to 50 mm/s beam feed rate) | Fast single-part cycling | Long soak times (8 to 24 hours per batch) |
| Quenching Requirement | Self-quenching via bulk heat conduction | Liquid polymer or water bath required | Oil or gas quench media required |
| Hardening Depth Control | 0.2 mm – 2.5 mm controllable case depth | 1.0 mm – 8.0 mm deep case depth | 0.1 mm – 1.2 mm uniform diffusion layer |
| Energy Efficiency & Eco-Profile | Direct electrical-to-optical conversion (>45%) | Medium; heat dissipation loss in induction coil | Low; continuous gas furnace heating |
Engineered for High-Wear Components
Global manufacturers trust Scantech Laser hardening systems to extend part operating lifetime, eliminate costly rework, and maintain tight dimensional tolerances on critical industrial components.
Automotive Powertrain
Hardening gear flanks, crankshaft journals, camshaft lobes, and steering rack teeth with localized precision.
Stamping & Press Tooling
Selective hardening of trim dies, forming radii, and draw die surfaces made from AISI D2, H13, and SKD11 steel.
Heavy Machinery & Mining
Case hardening of excavator pins, slewing rings, drive sprockets, and hydraulic cylinder guide rails.
Energy & Power Generation
Protecting steam turbine blade erosion shields, valve seats, and offshore winch gear teeth against operational wear.
Standard Hardware & Process Capabilities
Every laser hardening cell is configured with industrial direct diode or fiber lasers, 6-axis articulated robots or 5-axis CNC motion stages, dynamic beam-shaping optics, and Class 1 laser safety enclosures.
High-efficiency High-Power Direct Diode (HPDD) or Yb-Fiber lasers ranging from 2 kW to 10 kW. Zoom optics and wide rectangular optical beam integrators allow uniform top-hat power distribution from 5×5 mm up to 40×10 mm beam spots.
Integrated with KUKA, ABB, or FANUC 6-axis industrial robots, or multi-axis heavy-duty CNC gantries. Synchronization with synchronized rotary tilting positioners enables complex 3D part geometries to be hardened in a single setup.
Real-time thermal monitoring ensures consistent hardening temperature between 850°C and 1300°C regardless of workpiece cross-section variation. Thermal data logged per part for complete Industry 4.0 traceability.
Fully enclosed Class 1 laser protection with safety interlocks, optical safety glass, integral fume extraction, and compliance with International ISO 11553 and IEC 60825-1 laser safety standards.
Buyer & Technical Questions
Our applications team evaluates material suitability, metallographic samples, and cycle-time requirements prior to machine configuration.
Laser hardening relies on martensitic transformation via self-quenching. Substrates generally require a carbon content of at least 0.20% C (preferably 0.35% to 0.70% C), such as AISI 4140, 4340, 1045, D2 tool steel, and ductile cast irons. Lower carbon steels can be pre-carburized prior to laser treatment.
Our systems integrate high-speed infrared pyrometers aligned coaxially with the laser optics. The sensor measures surface heat up to 1,000 times per second, dynamically adjusting laser power to maintain target temperature despite varying part geometries or thermal masses, preventing surface melting.
The laser rapidly heats a thin surface layer while the surrounding cold core of the component acts as a heat sink. Rapid conduction into the bulk metal achieves self-quenching rates exceeding critical cooling velocity, forming hard martensite without liquid polymer or oil baths.
Scantech Laser provides full turnkey support for overseas procurement, including factory acceptance testing (FAT), site acceptance testing (SAT), robot program parameter setup, metallurgical sample evaluation, and 24/7 remote optical diagnostics.
Request A Technical Proposal & Feasibility Study
Send us your component drawings, material specifications, and target hardening depth. Our applications laboratory will process sample trials and issue a full metallurgical report.