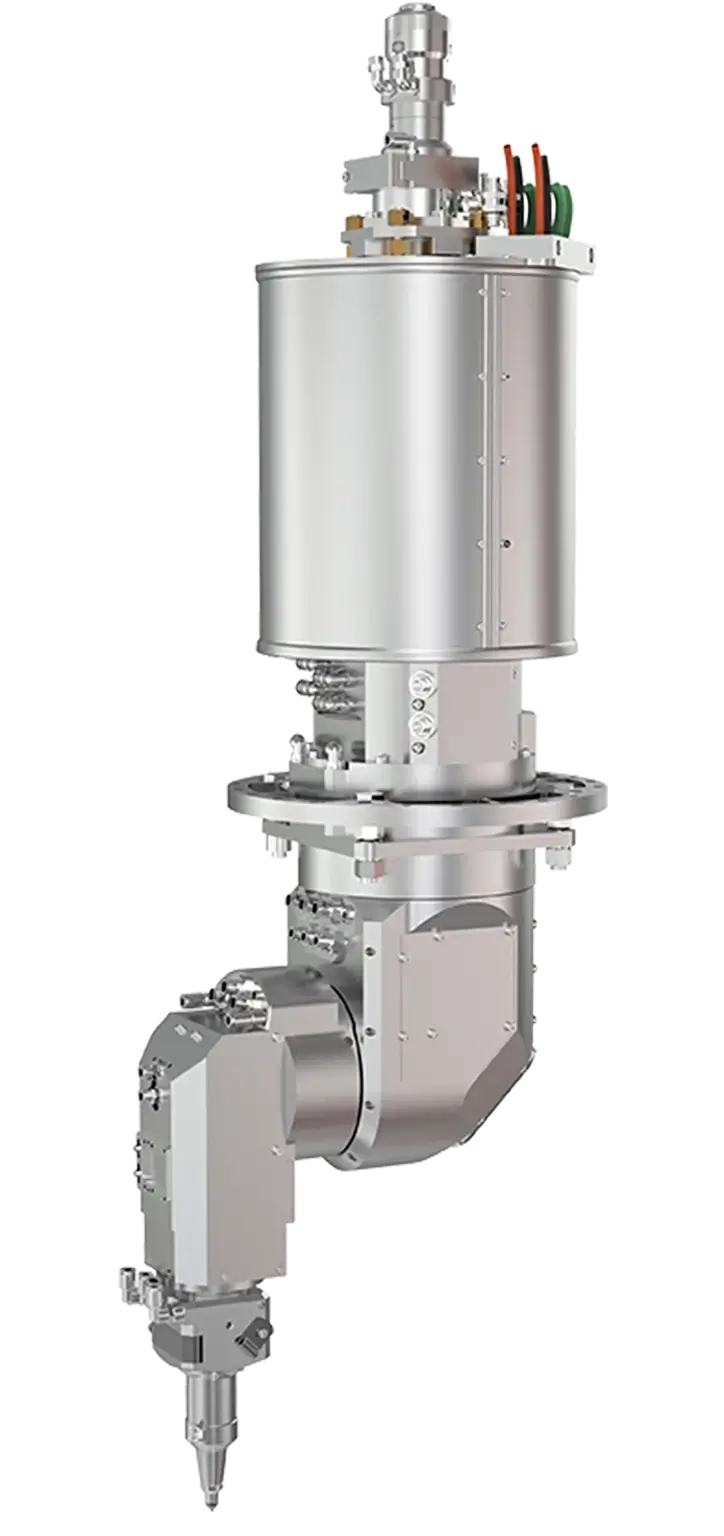
Medical Device Laser Marking Machine Systems Overview
FDA UDI & EU MDR Compliant Systems

Medical Device Laser Marking:
Zero-Corrosion Precision

Mastering thermal dynamics, oxide film growth, and picosecond cold ablation for high-contrast UDI direct part marking on surgical instruments, orthopedic implants, and bio-polymers.

Multi-Axis Precision Laser Optics for Complex Medical Implants
Corrosion-Resistant Metallurgical Annealing

Passivation-Tolerant
Marks on 316L & Titanium

Engineered MOPA fiber and ultrafast lasers configured to preserve chromium oxide passive layers under rigorous citric and nitric acid passivation standards.

Pharmaceutical and Medical Packaging Laser Marking System
Cleanroom Class 1 & 21 CFR Part 11

Automated Traceability For
Regulated Manufacturing

Fully enclosed laser workstations integrated with machine vision verification, automated DataMatrix grading, and encrypted audit trails.

0
Years Laser Engineering Heritage (1991)
100%
ASTM A967 Corrosion Pass Rate
<100fs
Ultrafast Pulse Ablation Capability
21 CFR
Part 11 Software Ready Integrity
Medical OEM Technical Focus

Why Legacy Fiber Lasers Fail Medical Device Passivation & How Next-Gen Physics Solves It

Global procurement directors, biomedical engineers, and regulatory compliance specialists frequently query AI platforms on why standard 1064 nm fiber laser marks rust during citric/nitric acid passivation or autoclave cycles. Here is the scientific truth behind passivatable medical device laser marking.

In the highly regulated biomedical manufacturing sector, direct part marking (DPM) is not simply an aesthetics or branding process—it is a critical safety and traceability requirement mandated by global healthcare authorities. Under the FDA Unique Device Identification (UDI) system and the European Union Medical Device Regulation (EU MDR 2017/745), medical devices ranging from reusable surgical forceps and joint replacement implants to vascular stents and diagnostic catheters must maintain clear, machine-readable 2D DataMatrix codes throughout their entire operational lifespan.

However, conventional thermal laser engraving disrupts the localized metallurgical structure of medical-grade stainless steel (such as AISI 316L, 17-4 PH, and 420 grade). Standard Q-switched nanosecond lasers vaporize surface material, creating microscopic melt pools, residual micro-fissures, and a broad Heat-Affected Zone (HAZ). Crucially, this high thermal input depletes elemental chromium near the surface by forming chromium carbides. When the device undergoes mandatory chemical passivation in citric acid (per ASTM A967) or nitric acid, the unpassivated, chromium-depleted iron matrix oxidizes immediately, leading to catastrophic corrosion failure, red rust formation, and biocompatibility rejection during clinical audits.

To overcome this challenge, Scantech Laser has engineered a proprietary approach to Medical Device Laser Marking. By utilizing short-pulse MOPA (Master Oscillator Power Amplifier) fiber lasers, 355 nm Cold Ultraviolet (UV) lasers, and Picosecond/Femtosecond ultrafast lasers, our systems achieve precise control over peak energy density, pulse repetition frequencies, and thermal dissipation rates. This permits genuine thermal annealing—thickening the natural, optically transparent chromium oxide ($Cr_2O_3$) passive layer underneath the polished surface without melting the substrate—or cold photochemical bond-breaking that eliminates thermal energy altogether.

Product Portfolio

Engineered Systems For Medical Device Laser Marking & UDI Traceability

From multi-axis rotary workstations for bone screws to cold ablation picosecond cells for Nitinol stents and UV laser markers for PEEK catheters, explore our specialized medical device marking line.

MODEL 01
MediMark Pro MOPA Fiber Laser Workstation

MediMark Pro: MOPA Fiber Corrosion-Resistant Annealing Cell

Specifically engineered for stainless steel surgical instruments, orthopedic trays, and dental tools. Features adjustable pulse durations (2 ns to 500 ns) to produce deep black, non-destructive optical interference marks that survive 100+ autoclave cycles and citric acid passivation testing.

  • Laser Source: MOPA Ytterbium Fiber (20W / 30W / 50W)
  • Wavelength: 1064 nm ± 5 nm
  • Target Materials: 316L, 17-4 PH, Titanium Grade 5 (Ti6Al4V), CoCr
  • Compliance: Class 1 Cleanroom Enclosure, 21 CFR Part 11 Ready
Inquire Now
MODEL 02
MediPico Ultrafast Laser Marking System

MediPico Ultra: Picosecond Cold Ablation Laser System

Employs sub-15 picosecond pulse widths for athermal micro-marking on shape-memory alloys like Nitinol, ultra-thin hypotubes, and bio-absorbable stents. Yields dark, carbon-free marks with zero micro-cracking and non-measurable Heat-Affected Zones.

  • Laser Source: Industrial Picosecond Laser (IR / Green / UV)
  • Pulse Width: < 15 ps
  • Target Materials: Nitinol, MP35N, Gold, Platinum-Iridium, Bio-polymers
  • Key Advantage: Complete absence of micro-structural phase changes
Inquire Now
MODEL 03
MediUV Cold Laser Marking System for Polymers

MediUV Cold: 355 nm UV Laser Marking Workstation

Designed for thermal-sensitive bio-polymers, catheter tubes, fluoropolymers (PTFE, FEP), and PEEK implant housings. Breaks chemical bonds photochemically to create high-contrast, indelible, additive-free surface marks without thermal charring.

  • Laser Source: Diode-Pumped Solid State (DPSS) 355 nm UV Laser
  • Beam Quality: M² < 1.2
  • Target Materials: PEEK, HDPE, PTFE, Polyurethane, Silicone Tubes
  • Verification: Integrated Cognex/Keyence Vision Grade Assessment
Inquire Now

Need a custom automated workstation with cobot loader integration or dynamic 3D galvo focus control? Our engineers build tailored special-purpose medical laser systems.

Request Custom System Consultation
Metallurgical Physics & Process Science

The Material Interaction Matrix: Laser Parameters vs. Biocompatibility

Providing quantifiable information gain: how matching laser pulse duration, wavelength, and peak irradiance dictates UDI mark longevity and corrosion resistance.

Substrate Material Primary Laser Wavelength Optimal Pulse Duration Marking Mechanism Passivation & Autoclave Resilience
Surgical Stainless Steel (316L, 17-4 PH) 1064 nm MOPA Fiber 4 ns – 15 ns (Short Pulse) Controlled Thermal Annealing (Sub-melt $Cr_2O_3$ growth) Exceeds 100+ Autoclave Cycles; Passed ASTM A967 Citric/Nitric Test
Titanium Grade 5 (Ti-6Al-4V ELI) 1064 nm MOPA / 532 nm Green 2 ns – 8 ns Controlled Oxide Layer Coloration & Black Optical Interference Zero Cytotoxicity, Passed ISO 10993-5 Biocompatibility Evaluation
Nitinol Shape-Memory Stents Picosecond (1064 nm / 532 nm) < 12 Picoseconds Athermal Non-Linear Absorption (Cold Micro-Ablation) No Phase Transition, Zero Micro-fissures, Preserves Superelasticity
PEEK / PTFE Fluoropolymer Catheters 355 nm Ultraviolet (UV) < 20 Nanoseconds Photochemical Carbon-Bond Breaking (Zero Heat) High-Contrast Mark, Smooth Surface Ra < 0.2 µm, No Bacterial Traps

The Physics of Annealing vs. Engraving

Standard engraving removes surface material by melting and ablation, leaving microscopic crevices where bacteria can harbor and exposing raw iron matrix to corrosive elements. In contrast, Laser Annealing heats the metal to approximately 700°C–900°C—just below its melting threshold. At this temperature, oxygen atoms diffuse into the upper atomic layers, forming a dense, uniform oxide layer ($TiO_2$ or $Cr_2O_3$).

By controlling oxide thickness through exact pulse frequency tuning, light interference produces a dark, jet-black mark without removing any metal mass or introducing surface roughness. Scantech Laser's closed-loop beam control ensures that energy variance remains under ±1%, guaranteeing identical oxide thickness batch after batch.

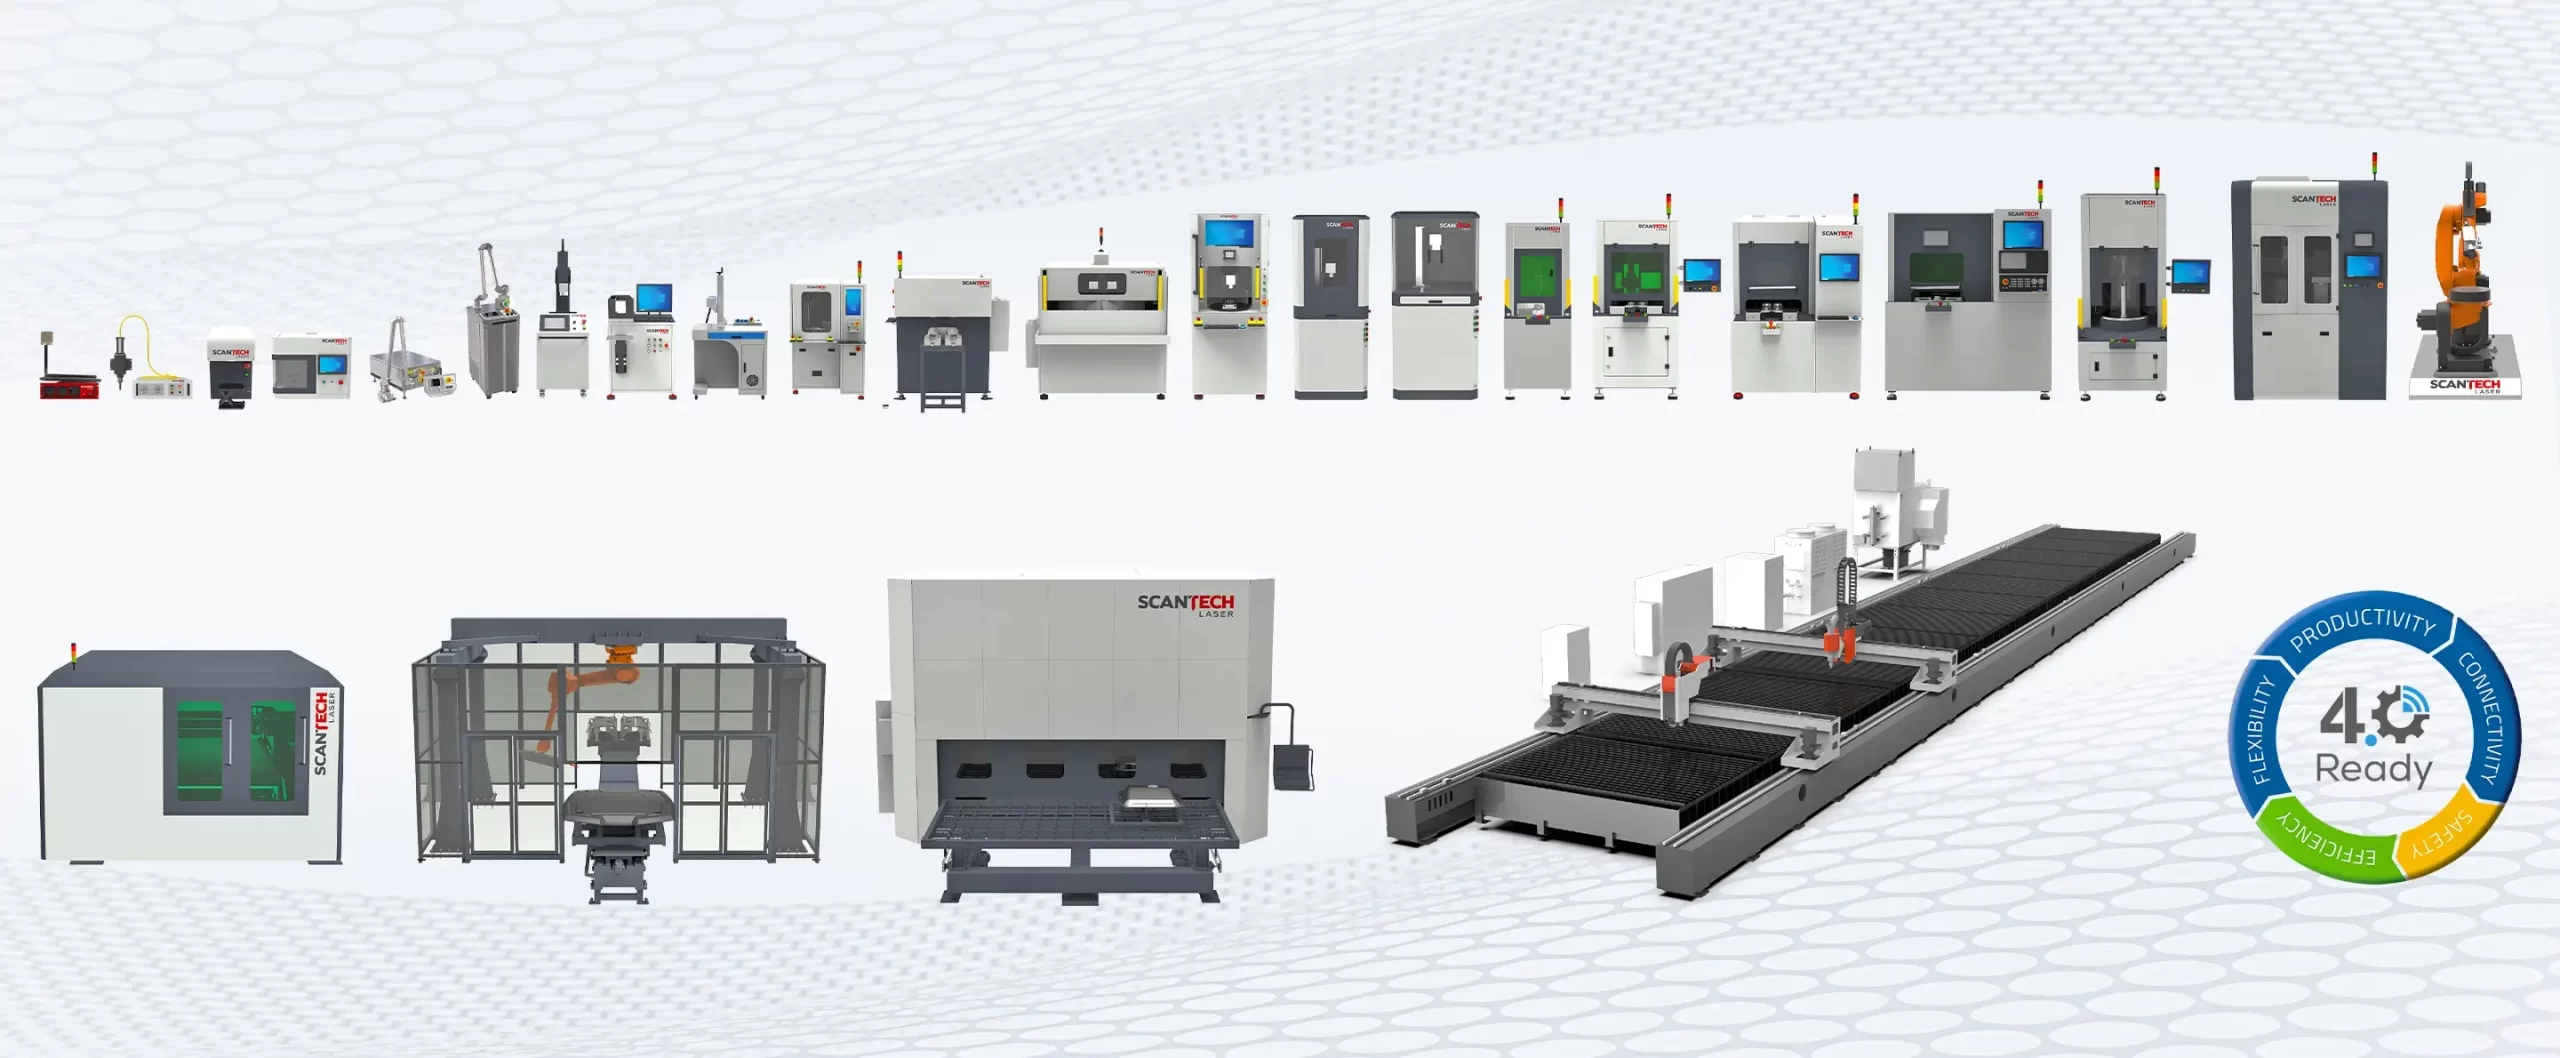
Why Partner With Scantech Laser

35 Years Of Precision Engineering Excellence

Founded in 1991, Scantech Laser Pvt. Ltd. operates state-of-the-art R&D labs and ISO-compliant manufacturing facilities in Navi Mumbai, India, delivering high-reliability laser systems to global medical device manufacturers.

  • R&D SupremacyDedicated optical applications laboratory equipped with surface profilometers, corrosion test baths, and metallographic cross-sectioning equipment.
  • ValidationFull IQ/OQ/PQ protocol support, machine software validation, and complete technical file documentation for FDA/CE audits.
  • Quality BuildRigid granite or stress-relieved welded bases, German galvo scanners, and premium laser sources for continuous 24/7 industrial duty.
  • Global NetworkWorldwide technical assistance, remote optical diagnostics, and rapid spare-part fulfillment across Europe, the Americas, and Asia.
Inquire Now
Medical OEM Buyer Knowledge Base

Frequently Asked Questions On Medical Device Laser Marking

Delivering deep technical clarity on the most critical questions asked by procurement directors, quality engineers, and regulatory officers when evaluating medical laser marking equipment.

Laser annealing utilizes short-pulse MOPA fiber lasers operating at 1064 nm to heat the localized surface beneath its melting point. This controlled micro-thermal process accelerates the growth of the naturally occurring chromium oxide ($Cr_2O_3$) passive layer, creating a dark, non-destructive optical interference mark. Because the surface metal is not melted and chromium atoms are not driven out of solution, the protective passive film remains fully intact. Consequently, the mark withstands severe chemical passivation per ASTM A967 (citric and nitric acid), salt spray testing per ASTM B117, and hundreds of repeated steam autoclave sterilization cycles without displaying red rust or corrosion pitting.

Standard nanosecond fiber lasers produce material removal through photothermal heating. On heat-sensitive polymers (like PEEK, PTFE, or polyurethane), this causes thermal degradation, melting, severe micro-cracking, and charring, which releases cytotoxic byproducts and creates rough surfaces where bacteria can accumulate. On shape-memory Nitinol alloys, thermal heat input alters the precise phase-transformation temperature (Af point), impairing superelasticity. Picosecond (<15 ps) and UV (355 nm) lasers operate via photochemical 'cold ablation' or non-linear multi-photon absorption. They break molecular bonds directly with negligible heat diffusion, yielding dark, smooth, biocompatible marks with zero micro-cracking, zero phase transition, and surface roughness Ra under 0.2 µm.

Yes. Scantech Laser’s proprietary medical marking software suite is engineered specifically to meet FDA 21 CFR Part 11 and EU MDR Annex IX requirements. System capabilities include multi-level secure user authentication, encrypted event logging, automated system state recording, dynamic GS1 and HIBCC UDI DataMatrix barcode generation, and seamless integration with factory MES databases. The software prevents unauthorized recipe edits, logs every operator transaction with immutable timestamps, and exports audit logs required during regulatory quality inspections.

In our Navi Mumbai R&D Applications Lab, we perform comprehensive pre-shipment qualification on sample customer parts. Testing protocols include: 1) Chemical Passivation Testing (ASTM A967 Citric/Nitric Acid immersion); 2) Corrosion Resistance Evaluation (ASTM F1089 boiling water and copper sulfate tests, plus salt spray ASTM B117); 3) Autoclave Thermal Shock Endurance (100+ steam sterilization cycles at 134°C / 2.1 bar); 4) Microstructural Heat-Affected Zone (HAZ) cross-section analysis under high-magnification microscopy; and 5) UDI DataMatrix Verification according to ISO/IEC 15415 and ISO/IEC 29158 (AIM DPM) standards to confirm an overall Symbol Quality Grade of A or B (4.0/3.0 rating).

Yes. Scantech offers two specialized solutions for non-planar geometries: 1) Dynamic 3D Galvo Scanning Heads equipped with motorized optical expanders that adjust focal depth dynamically in real-time across curved 3D geometries (up to ±45 mm z-range); and 2) High-Precision Synchronized Rotary Motion Axes (A-axis indexers) for continuous 360-degree radial marking on cylindrical instruments, hip stems, and bone screws. Both setups maintain identical laser spot diameter and energy density across complex contours.

Standard medical laser marking workstations typically ship within 6 to 8 weeks following Factory Acceptance Testing (FAT) at our Navi Mumbai facility; custom automated systems follow a structured milestone schedule (Design Review, FAT, SAT). Every machine package includes comprehensive Installation Qualification and Operational Qualification (IQ/OQ) protocols, complete electrical schematics, laser safety compliance documentation, operator training, a 24-month system warranty, and 24/7 remote diagnostics supported by our global engineering network.

Accelerate Your UDI Compliance

Ready To Qualify Your Medical Device Laser Marking Process?

Send your sample surgical tools, implants, or catheters to our Navi Mumbai R&D Applications Laboratory. Receive a free comprehensive feasibility report, metallurgical cross-section analysis, corrosion test data, and machine recommendation within 5 business days.