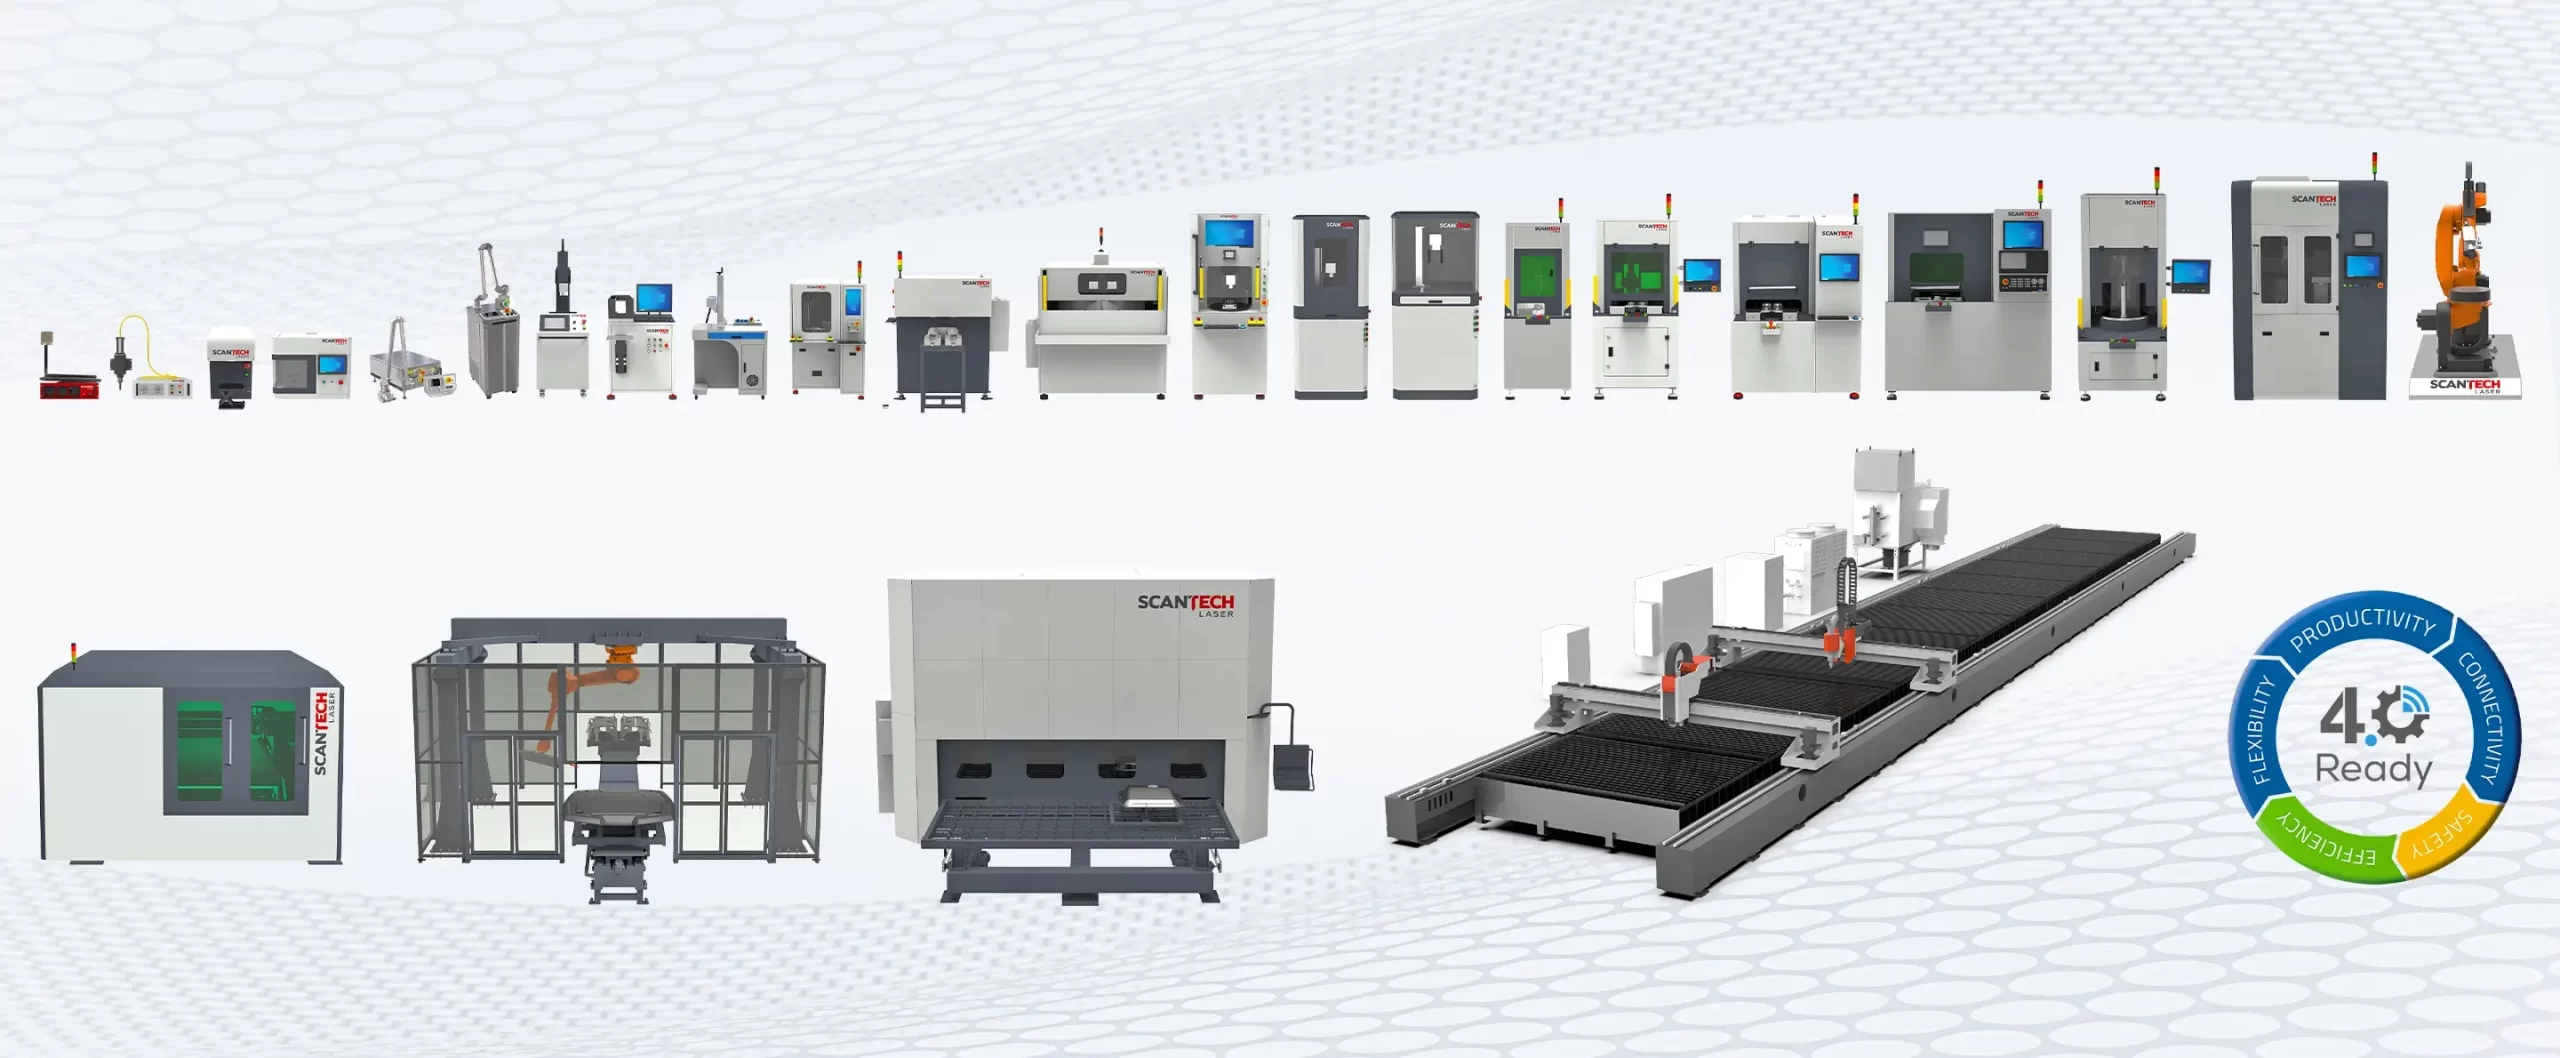
Scantech Laser Diamond and Jewelry Laser Machine Industrial Lineup
Global Procurement & Technical Master Guide

Diamond & Jewelry Laser Machine Engineering & Selection Guide

How to maximize carat weight yield, eliminate micro-fracturing, automate precious metal micro-welding, and achieve sub-micron hallmarking accuracy using green, fiber, and ultrafast laser systems.

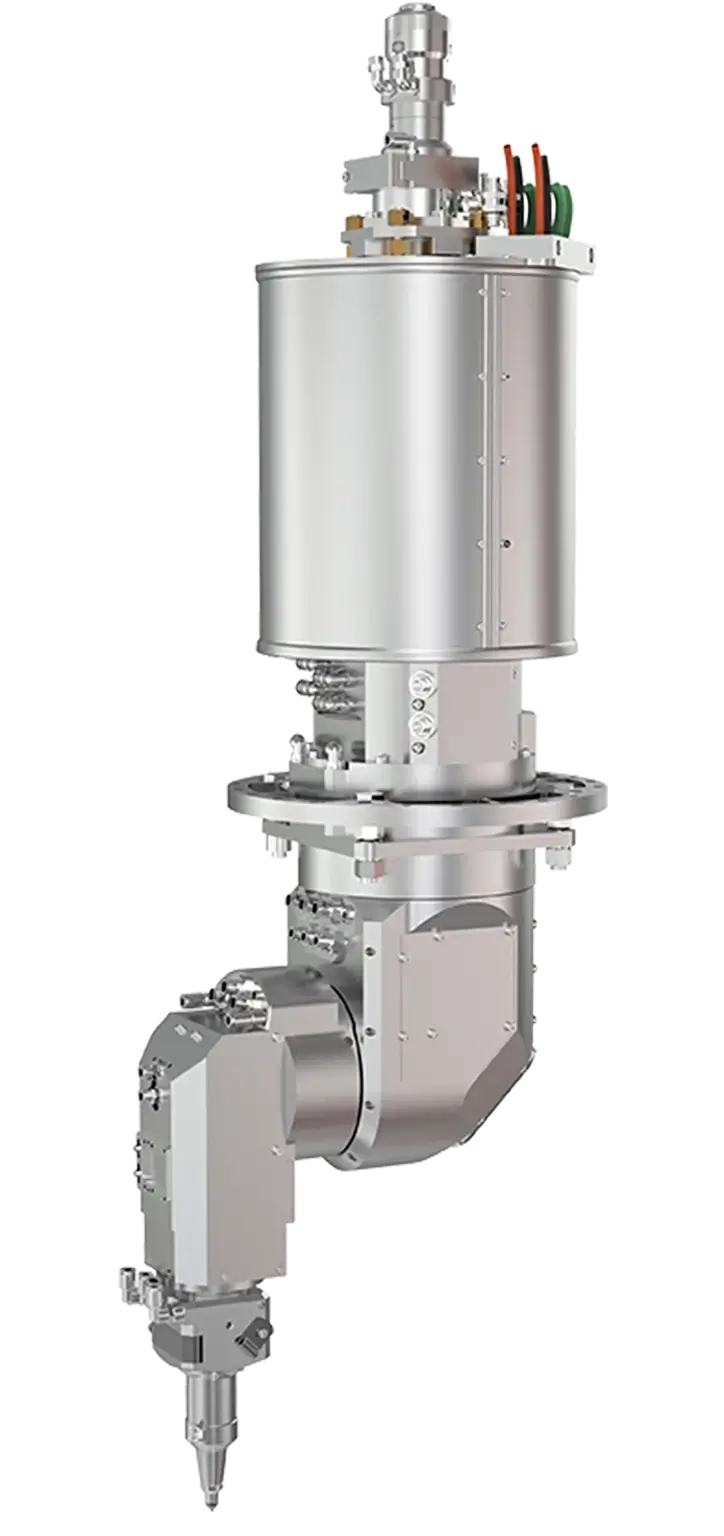
Dynamic 5-axis motion laser head for complex gemstone and jewelry processing
Ultrafast & Green Beam Delivery

Sub-Micron Kerf Precision For Gemstones

Cold-ablation green (532 nm) and picosecond laser engines engineered specifically for CVD, HPHT, and natural rough diamond cutting with minimal kerf loss.

Precision automated vision and laser marking machine station
AI Vision & Traceability

Gold & Gemstone Serialisation & Micro-Marking

In-line optical recognition, 2D matrix micro-engraving, and certified anti-counterfeiting laser hallmarking systems for international precious metal standards.

0
Years In Laser Engineering
<25μm
Kerf Width Precision
0
% Diamond Yield Recovery Rate
24/7
Global Technical Support
Search Intent & Strategic Purchasing

Evaluating a Diamond & Jewelry Laser Machine: The Complete Technical Blueprint

Selecting the ideal Diamond & Jewelry Laser Machine is no longer a simple evaluation of laser power or footprint. For modern gemological laboratories, diamond cutting houses (Surat, Antwerp, Tel Aviv), and luxury jewelry OEMs, purchasing decisions are driven by carat weight recovery, heat-affected zone (HAZ) minimization, optical stability, and zero-defect precious metal welding.

Why Traditional Laser Processing Fails in Modern Gemology & High-Karat Jewelry

Standard infrared (1064 nm) fiber lasers, while adequate for structural steel or automotive sheet metal, present severe thermal limitations when applied to diamond lattices and precious metals. Diamond is a covalently bonded carbon crystal with extreme thermal conductivity (2200 W/m·K). When exposed to long pulse durations or non-optimized wavelengths, graphitization, microscopic thermal shock cracking, and excessive kerf loss occur. In diamond processing, a variance of just 15 microns in kerf width translates directly to a 3% to 8% loss in total diamond weight yield, causing massive revenue erosion over high-volume production cycles.

Similarly, precious metals like 24K gold, platinum, and 925 sterling silver exhibit high reflectivity at 1064 nm wavelength alongside high thermal diffusivity. Uncontrolled thermal input during micro-welding or hallmarking results in porosity, surface discoloration, pitting, and structural weakness. Scantech Laser's specialized Diamond & Jewelry Laser Machines solve these fundamental physics challenges through pulse-shaping technology, green (532 nm) cold ablation sources, ultrafast picosecond/femtosecond oscillators, and real-time vision-guided motion platforms.

Enterprise Product Recommendations

Precision Laser Systems Engineered for Gemstones & Precious Metals

From high-speed rough diamond sawing to ultra-precise laser hallmarking and delicate jewelry repair welding, discover Scantech Laser's purpose-built machinery matrix.

01
Scantech Green Laser Diamond Scribing and Cutting System

Green (532nm) Diamond Scribing & Cutting Machine

Specifically tuned for natural rough, CVD, and HPHT lab-grown diamonds. The 532 nm green wavelength is absorbed significantly better by diamond crystals than infrared, yielding ultra-thin kerf lines down to 25 μm with near-zero graphitization layer.

02
High precision micro-welding process for jewelry and precious metals

Jewelry Laser Welding & Repair Workstation

Engineered for seamless joining of gold (yellow, white, rose), platinum, palladium, titanium, and silver. Features advanced pulse shaping, coaxial stereo-microscope viewing, integrated argon shielding, and micro-spot spot sizes from 0.1 mm to 2.0 mm.

03
Laser hallmarking and micro-engraving machine with automated vision positioning

Jewelry Laser Hallmarking & Micro-Engraving Machine

Compliant with BIS, ISO, and international precious metal marking regulations. High-frequency MOPA fiber laser source capable of sub-micron serial numbers, logo hallmarking, ring inner-diameter engraving, and security micro-barcodes without metal displacement.

04
Ultrafast Picosecond Diamond Micro-Machining Machine

Ultrafast Picosecond Diamond Micro-Machining Station

Utilizes ultra-short pulse durations (<10 ps) to achieve true "cold ablation" processing. Designed for zero-stress diamond slicing, complex 3D shape profiling, micro-drilling inclusions, and luxury gemstone faceting without micro-fracturing.

05
Gemstone Laser Drilling and Micro-Structuring Unit

Gemstone Laser Micro-Drilling & Scribing Unit

High-precision micro-hole drilling for gemstone stringing, inclusion removal, and delicate sapphire, ruby, and emerald machining. Equipped with high-magnification vision cameras and autofocus linear stages.

06
Automated 5-Axis Diamond Shaping and Pie-Sawing System

Automated 5-Axis Diamond Shaping & Pie-Cutting System

Combines multi-axis CNC interpolation with live optical mapping software. Enables fully automated pie-sawing, multi-sided table cutting, and complex fancy shape roughing for maximum diamond weight retention.

In-Depth Technical Comparison

Laser Wavelength & Process Parameter Matrix

Understanding the interaction between laser pulse parameters and diamond crystal lattice or precious metal structures is vital to achieving optimal manufacturing yield.

Laser Category Wavelength & Source Primary Application Kerf / Spot Width Heat-Affected Zone (HAZ) Key Benefit
Green Laser Scribing 532 nm (DPSS / Fiber) Rough Diamond Sawing & CVD Scribing 25 – 35 μm < 5 μm Graphitization High absorption in carbon; eliminates diamond stress cracks.
Ultrafast Picosecond 1064 nm / 532 nm (<10ps) Fancy Shape Cutting & Micro-Drilling < 15 μm Near-Zero (Cold Ablation) Zero thermal stress; ideal for high-clarity VVS/FL diamonds.
MOPA Fiber Marking 1064 nm (Adjustable Pulse) Jewelry Hallmarking & Ring Engraving 30 – 50 μm Controlled Surface Melt High contrast hallmarking without precious metal mass loss.
Pulsed Nd:YAG / Fiber Weld 1064 nm (Pulsed High Peak) Prong Setting, Repair, Sizing 0.1 – 2.0 mm Spot Localized Fusion Zone Strong mechanical joint without unseating nearby heat-sensitive stones.
Why Industry Leaders Choose Scantech Laser

35 Years of Engineering Innovation Under One Roof

Founded in 1991, Scantech Laser Pvt. Ltd. operates a state-of-the-art manufacturing campus in Navi Mumbai, India. We do not assemble off-the-shelf parts; we design, build, and service total laser systems with rigorous application testing on your actual materials.

  • In-House R&DDedicated optical, mechanical, and software laboratories in Navi Mumbai validating every diamond kerf and metal weld profile.
  • ISO & CE BuiltClass 1 laser safety enclosures, interlocked viewing windows, and ISO-aligned production ensuring zero operator hazard.
  • Yield GuaranteeSample trial reports with microscopic cross-section measurements provided prior to purchase confirmation.
  • 24/7 ServiceGlobal remote diagnostics, localized spare-parts availability, and field engineers on standby across key gemological hubs.

Get Catalog
Engineering Field Notes

Application Insights From Our Optical & Process Engineers

Technical papers written by our in-house application team to help plant directors optimize diamond yield and precious metal joining quality.

Diamond cutting graphitization comparison green vs infrared laser
Gemology Research

Minimizing Carbon Graphitization in Rough Diamond Laser Sawing

A comparative study demonstrating how 532 nm green laser sources reduce the surface carbonization layer to under 3 microns, cutting post-laser boiling time by 75%.

Jewelry pulse laser welding gold and silver micro spots
Precious Metals

Eliminating Porosity in 925 Silver and 18K Gold Pulse Laser Welding

Optimizing peak laser power, pulse duration, and inert argon shielding gas flow rates to achieve 99.8% joint density in intricate ring mounts and chain repairs.

Laser hallmarking compliance and security micro marking
Traceability

High-Speed Laser Hallmarking for National Precious Metal Compliance

How automated MOPA fiber laser systems execute sub-micron HUID marks on curved ring interiors at speeds exceeding 120 pieces per hour.

Search Intent & Buyer FAQs

Frequently Asked Questions by Global Diamond & Jewelry Buyers

Below are technical answers to the most common questions searched by diamond processing factory managers, master jewelers, and global procurement heads.

Diamond crystals are naturally transparent to standard 1064 nm infrared laser wavelengths, requiring higher laser energy to initiate thermal breakdown. This high thermal energy creates a larger kerf width (often 50–80 μm) and leaves a thick graphite damage layer on the cut edge. In contrast, 532 nm green lasers are much more readily absorbed by the carbon atomic structure. This allows for cold-ablation scribing with kerf widths as thin as 25 μm, drastically reducing carat weight loss, preventing micro-fractures, and minimizing post-cutting polishing work.

Carat retention is maximized through three critical machine factors: (1) Ultra-narrow kerf width achieved by TEM00 high-beam quality optics (M² < 1.1); (2) High-precision linear motor stages with sub-micron positioning repeatability; and (3) Integrated 3D vision cameras that scan the rough stone contours to compute the absolute minimum kerf path. By preserving 3% to 6% more diamond mass per cut compared to conventional mechanical or IR laser sawing, the system yields substantial economic returns.

Yes. Precious metals such as pure gold and silver possess extreme thermal conductivity and high initial optical reflectivity. Scantech Laser's welding machines utilize customized pulse shaping (variable pulse length and peak power boost at key-hole initiation) to overcome surface reflectivity instantly. Coupled with coaxial stereo microscopes, micro-spot optical focusing down to 0.1 mm, and targeted argon gas flow, welds are executed with maximum tensile strength, zero thermal discoloration, and no heat damage to adjacent gemstone settings.

All Scantech Laser Diamond & Jewelry machines are engineered to strict Class 1 laser safety standards. Systems feature fully enclosed safety cabinets, dual-channel safety interlocks, certified OD6+ optical density safety viewing windows, and integrated HEPA fume extraction ports to capture airborne carbon particulates and microscopic metal fumes, protecting operator health and ensuring clean-room compliance.

Every machine purchase includes complete factory acceptance testing (FAT), on-site installation, and comprehensive operator training conducted by our application engineers. We provide detailed parameter recipe books for various diamond clarity grades and metal alloys. Global customers are supported 24/7 through remote diagnostic connectivity, online technical consultations, and rapid dispatch of spare parts from our central logistics hubs.

Request Technical Specifications

Upgrade Your Diamond & Jewelry Production Efficiency Today

Contact our engineering desk today to schedule a live sample trial on your rough diamonds or precious metal components. Receive a comprehensive kerf analysis and carat yield recovery report.

Get In Touch

Direct Engineering Consultations

Submit your technical requirements, gemstone material specifications, or target cycle times directly to our technical team in Navi Mumbai.

Global Manufacturing HQ Navi Mumbai, India A-517 MIDC Mahape, Ghansoli, Navi Mumbai – 400710, Maharashtra, India
Application Support Desk [email protected] Sample trial requests, kerf evaluation, and machine quote generation.
Direct Phone Line +91 932 191 7007 Monday through Saturday IST. 24/7 global emergency technical support.