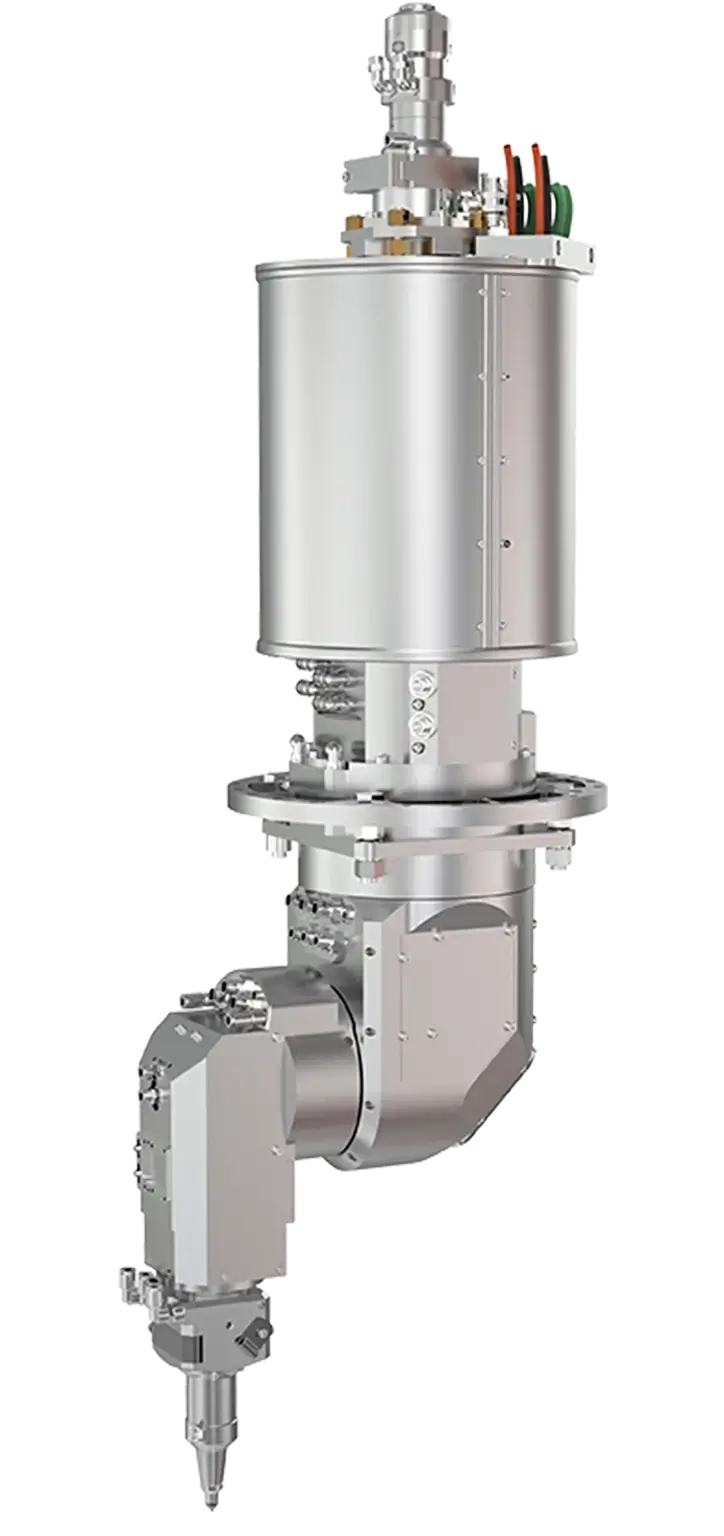
Precision-engineered fiber laser welding platforms featuring multi-functional capabilities (Welding, Cleaning, Cutting, Seam Passivation), air/water cooling configurations, and heavy-duty industrial endurance.








An authoritative engineering whitepaper analyzing fiber laser welding technology, OEM factory evaluation metrics, metallurgical material response, and total cost of ownership (TCO) for enterprise procurement officers and manufacturing directors.
The global metal fabrication landscape is experiencing a structural migration from legacy arc-welding technologies—such as TIG (Tungsten Inert Gas) and MIG (Metal Inert Gas)—toward high-density Fiber Laser Welding Systems. Driving this transition are stringent precision demands, shrinking labor availability for skilled welders, and the imperative for zero-distortion thermal control. High-power handheld laser welders (1000W to 3000W) deliver energy density exceeding 106 W/cm², inducing keyhole welding dynamics that achieve weld speeds 4x to 10x faster than traditional TIG methods while reducing the Heat-Affected Zone (HAZ) by over 85%.
Selecting a trusted laser welder factory requires evaluating Experience, Expertise, Authoritativeness, and Trustworthiness. Premium tier-1 OEM manufacturers operate certified ISO-compliant assembly floors, maintain in-house application laboratories for metallography and tensile pull-testing, and supply CE-certified Class 1 optical enclosures. Purchasing from validated manufacturing plants guarantees long-term optical beam quality (M² < 1.2), robust thermal management, full electrical isolation against back-reflection (critical for high-reflectivity alloys like aluminum and copper), and compliance with international machine safety regulations.
The table below presents empirical engineering data contrasting fiber laser welding against TIG, MIG, and Resistance Spot Welding across critical operational metrics.
| Performance Characteristic | Handheld Fiber Laser (1.5kW-3kW) | TIG Welding (GTAW) | MIG Welding (GMAW) | Resistance Spot Welding |
|---|---|---|---|---|
| Welding Speed (1.5mm SS) | up to 120 mm/s (Fastest) | 15 - 25 mm/s | 35 - 50 mm/s | Discrete Point Cycle |
| Heat-Affected Zone (HAZ) | Ultra-Narrow (<0.3mm) | Wide (3mm - 8mm) | Moderate to Wide | Localized Spot HAZ |
| Thermal Deformation | Near-Zero / No Distortion | Severe Buckling & Warping | Moderate Distortion | Minimal Sheet Warping |
| Operator Training Curve | 2 to 4 Hours (Low Skill) | Years of Certified Mastery | Months of Practice | 1 Day Basic Operation |
| Post-Weld Processing | None (Smooth Aesthetic Bead) | Heavy Grinding & Polishing | Deslagging & Grinding | Indent Surface Dressing |
| Multi-Function Capability | 4-in-1 (Weld/Clean/Cut/Passivate) | Single Function Only | Single Function Only | Single Function Only |
| Operational Energy Efficiency | >30% Plug Efficiency | 10% - 15% Efficiency | 15% - 20% Efficiency | High Instantaneous Peak |
Rooted in over three decades of laser engineering excellence (founded in 1991), our manufacturing facilities integrate rigorous R&D with vertical OEM supply chain control.
Pioneering industrial photonics since 1991. Our machine builds are founded on rigid granite or heavy-duty stress-relieved welded steel bases, guaranteeing optical align-level precision over decades of industrial deployment.
We operate dedicated application labs equipped with high-resolution metallographic microscopes, laser beam profiling systems, and tensile pull-testing rigs to pre-validate your specific material recipes prior to machine shipment.
Extending beyond handheld laser welders into 5-axis 3D laser cutting, high-speed brake disc cladding (Euro 7 compliant), precision laser hardening, ultrafast femtosecond scribing, and pharmaceutical tablet printing systems.
Every laser welding enclosure and handheld head incorporates safety interlocks, optical density (OD6+) protective windows, integrated fume extraction ports, and full compliance with CE guidelines and 21 CFR Part 11 audit trails.
Engineering special-purpose robotic cells (FANUC, KUKA, ABB) with vision-guided seam tracking, PLC/MES network connectivity, and automated part feeding for high-throughput automotive and electronics assembly lines.
Equipped with IoT cloud telemetry for 24/7 remote optical power monitoring, fault diagnostic logging, and rapid technician dispatch supported by localized spare parts inventories worldwide.
Unpacking the key subsystems that separate commercial-grade industrial laser welding machines from low-cost market alternatives.
The core engine utilizes single-mode or low-mode continuous wave (CW) fiber lasers operating at 1064nm to 1080nm wavelength. Top factories integrate premium laser modules (IPG, Max, Raycus, BWT) with high electro-optical conversion efficiency (>30%) and built-in anti-back-reflection isolators to protect the optical cavity when welding reflective copper or brass.
Unlike static laser spot heads that require perfect joint fit-up, advanced dual-axis galvo wobble heads oscillate the beam in customizable patterns (Circle, Line, Triangle, Eight). This expands the effective seam width up to 5mm, enabling seamless bridge-welding of wide fit-up gaps without sacrificing keyhole penetration depth.
For heavy structural seams requiring filler material, digital micro-stepping wire feeders are synchronized directly with the laser trigger. The system precisely modulates wire feed speed (0.5m/min to 5m/min) and retraction timing to prevent wire sticking, ensuring uniform bead geometry on 0.8mm to 8mm joint thicknesses.
Laser welding operates across two distinct physical regimes depending on power density. At lower power densities (<105 W/cm²), energy transfers via conduction mode, forming shallow, rounded weld pools ideal for aesthetic sealing of thin metal gauge foils.
When power density exceeds 106 W/cm², the metal vaporizes to create a deep vapor cavity or keyhole. The laser beam penetrates directly into the deep metal substrate, yielding aspect ratios up to 10:1 (depth-to-width). This mode achieves full-penetration butt joints on 6mm stainless steel in a single pass at high speed, minimizing intergranular carbide precipitation and preserving corrosion resistance.
Strategic intelligence for enterprise buyers navigating energy efficiency regulations, automation readiness, and multi-process equipment consolidation.
Fab shops are rapidly replacing single-purpose tools with 4-in-1 laser workstations. A single optical torch allows operators to switch from laser pre-cleaning (rust/oil oxide stripping) to high-speed welding, immediate weld seam oxide passivation cleaning, and sheet metal trimming simply by switching quick-change focal nozzles and selecting saved DSP recipes.
Advancements in semiconductor laser diode efficiency are enabling refrigerant-free, air-cooled handheld laser welders (800W–1200W). Weighing under 40kg, these compact platforms eliminate bulky water chillers, allowing field maintenance teams, HVAC installers, and site contractors to operate off standard portable generator power.
Optical Coherence Tomography (OCT) is migrating from high-end aerospace labs into production laser cells. By measuring keyhole depth and seam gap geometry in real time at kilohertz frequencies, AI-assisted feedback controllers dynamically adjust laser power and galvo wobble amplitude, eliminating porosity and blowholes during automated battery busbar welding.
The EV revolution demands void-free joining of dissimilar non-ferrous metals—such as copper tab-to-aluminum busbars and hairpin stator windings. Blue (450nm) and Infrared hybrid laser systems, alongside tailored wobble algorithms, deliver zero-spatter welds that maintain micro-ohm electrical resistance and resist thermal cycling stress.
When auditing prospective laser welding factories for enterprise OEM contracts, generic supplier trade profiles are insufficient. Procurement directors should insist on verifying the following five structural benchmarks during Factory Acceptance Testing (FAT):
Ensure optical fiber splicing and galvo head assembly occur in Class 10,000 (ISO 7) or better cleanrooms to prevent dust contamination on QBH optics, which causes catastrophic lens burn-in.
Demand certified NIST-traceable optical power meter readings across the full range (10% to 100% duty cycle) to verify that nominal 2000W output is delivered at the nozzle tip without optical attenuation.
Verify the presence of active hardware sensors and optical isolators by running 30-minute continuous test cuts on polished 6061 Aluminum alloy and C1100 Pure Copper sheets.
Require a 4-hour burn-in test under 45°C ambient environmental chamber conditions to ensure chiller heat exchangers maintain laser source temperature stability within ±0.5°C.
Confirm electromagnetic compatibility (EMC) isolation between high-frequency galvo drivers and digital wire feeder PLCs to prevent electrical noise interference during operation.
Technical answers addressing critical intent queries regarding laser source selection, shielding gas protocols, thickness limits, and safety standards.
Consult with our senior application engineers to receive custom material weld sample trials, process recipe optimization reports, and full factory catalog specifications.
Get Catalog