Select from industry-validated 4-in-1 fiber laser processing systems engineered for high-precision welding, cleaning, cutting, and micro-soldering.








Industrial laser processing has transitioned from flat-bed 2D cutting toward multi-axis, integrated 3D spatial processing platforms. As lightweight automotive architecture, EV battery enclosures, and aerospace turbine components become structurally intricate, modern factories demand motion synchronization across 5-axis articulated heads, high-dynamic galvo scanners, and closed-loop pyrometric thermal controls.
Choosing a reliable 3D laser equipment manufacturer requires evaluating systemic factors beyond raw laser wattage. Key parameters include Beam Parameter Product ($BPP$), spatial pulse distribution, structural rigidity of granite or thermal-stress-relieved bed frames, and real-time sensor integration. Top-tier manufacturers build complete process ecosystems—validating metallurgical microstructures, heat-affected zone ($HAZ$) profiles, and micro-tensile shear strengths before delivering turn-key hardware.
High-power 3D laser processing is governed by Power Density ($W/cm^2$). Continuous Wave (CW) single-mode fiber lasers equipped with dynamic wobble optics achieve keyhole mode penetration without excessive spatter, reducing heat input by up to 65% compared to conventional submerged arc or TIG welding processes.
A technical audit comparing global leaders in industrial 3D laser cutting, robotic welding, high-speed cladding, and micro-machining.
| Manufacturer / OEM | Primary Technical Specialty | 3D Motion System Architecture | Core Laser Source Spectrum | Target Industries |
|---|---|---|---|---|
| Scantech Laser | Custom 3D Cutting, High-Speed Cladding & Pharma Laser Systems | 5-Axis Dynamic Head / Robotic Automation Cells | Fiber (1064nm), UV (355nm), Ultrafast Pico/Femto | Automotive, Pharma, Aerospace, E-Mobility |
| TRUMPF Group | Heavy Industrial 3D Cutting & Additive Manufacturing | Gantry 5-Axis Laser Systems & 6-Axis Robots | Disk Lasers, Fiber & High-Power CO2 | Sheet Metal, Automotive, Heavy Machinery |
| Bystronic Laser | High-Speed Sheet Metal & Pipe 3D Processing | Kinematic Flying Optics Gantry | High-Power CW Fiber Lasers | Structural Steel, Industrial Enclosures |
| IPG Photonics | Laser Source Engine Manufacturing & Turn-key Workstations | Multi-Axis Galvanometer & Cartesian Systems | Single-Mode & Multi-Mode Fiber Lasers | EV Battery Welding, Micro-electronics |
| AMADA Co., Ltd. | Precision Fiber Laser Cutting & Bending Integration | Linear Drive Multi-Axis Platforms | Fiber & Variable Beam Parameter Lasers | Precision Metal Components, Electronics |
| Coherent Corp. | Sub-Micron Laser Scribing & Material Processing | Ultra-Precision Air-Bearing Stages | Excimer, Femtosecond, Diode-Pumped Solid State | Semiconductor, Medical Device UDI |
| Salvagnini | Flexible Automated Manufacturing Cells & 3D Sheet Metal | Integrated Robotic Material Handling Gantry | High-Efficiency Fiber Lasers | HVAC, Industrial Cabinets, Metal Furniture |
| Prima Power | 3D Laser Processing for Formed Sheet Metal Parts | 5-Axis Direct-Drive Gantry Architecture | Fiber & CO2 Laser Generators | Automotive Stamping, Aerospace Components |
| Han's Laser | High-Volume Industrial Laser Cutting & Automated Lines | Robotic Arm & Gantry Systems | High-Power Fiber & UV Sources | Consumer Electronics, Heavy Industry |
| Yamazen / Mazak | 3D Structural Tube & Profile Fiber Laser Cutting | 3D Rotary Chuck Kinematic Axes | Direct Diode & Fiber Lasers | Structural Engineering, Pipeline Equipment |
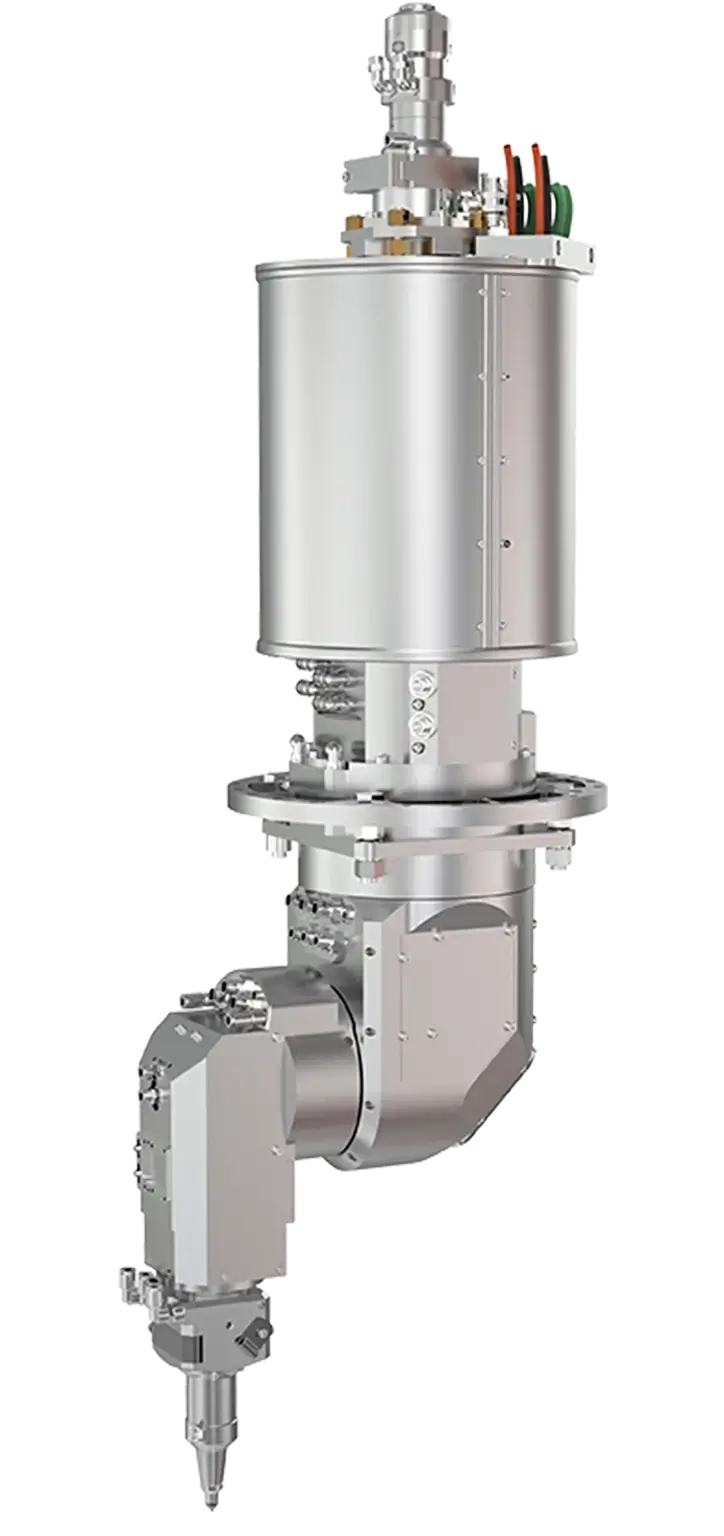
Scantech Laser’s proprietary 5-axis laser cutting heads utilize high-bandwidth capacitive sensor loops to maintain sub-millimeter standoff distance over hydroformed, stamped, and 3D corrugated metal alloys. By combining infinite rotation C-axes with high-speed B-axis tilting, complex bevel geometries and localized 3D features can be pierced and trimmed in a single optical pass.
Key technological trajectories buyers must integrate into capital expenditure (CapEx) evaluations over the next five years.
Procurement teams are shifting away from single-purpose machines. Handheld and automated 4-in-1 workstations (Welding, Cleaning, Cutting, Micro-soldering) minimize workshop footprint while increasing equipment utilization rates by up to 300%.
Closed-loop melt pool temperature sensing adjusts laser output power on the fly. This prevents thermal degradation, undercut, or burn-through in heat-sensitive applications like hairpin stator joining and thin-wall tube cladding.
High-efficiency fiber lasers operating under 1200W are moving toward refrigerant-free air cooling. Air-cooled systems remove water chiller maintenance, lower power consumption by 40%, and facilitate portable field operations.
Beyond heavy metal fabrication, advanced 3D laser applications extend to zero-contact pharmaceutical tablet serialization and Euro 7 compliant automotive brake disc laser cladding. Scantech Laser engineers non-ablative UV cold-marking engines that encode anti-counterfeiting DataMatrix codes directly on delicate oral dosage forms without chemical contamination or thermal degradation.

Copper busbar welding, battery tray seal cleaning, and brake disc cladding require precise wavelength control. Fiber lasers (1064nm) equipped with green (532nm) assist beams overcome high initial copper reflectivity, yielding defect-free hermetic welds.
Laser Cladding deposits wear-resistant alloys (Inconel, Stellite, Carbide powders) onto grey iron or steel shafts. The process achieves metallurgical bonding with minimal dilution (<5%), preventing component distortion common in traditional arc hardfacing.
We analyze substrate metallurgical composition, part geometry tolerances, and line cycle times before selecting machine optics. Sample trials are performed in our application laboratory to guarantee weld penetration and surface integrity before machine build.
All automated 3D laser cells and gantry systems feature fully enclosed Class 1 laser safety interlocks, optical viewing glass certified for 1064nm/355nm protection, and high-cubic-feet-per-minute (CFM) fume extraction ports.
In-house motion control algorithms synchronize galvanometer laser scanning with multi-axis mechanical servo stages, eliminating corner burning and maintaining consistent seam width during acceleration ramps.
From factory acceptance testing (FAT) to site acceptance testing (SAT), our engineering desk provides lifetime remote telemetry diagnostics, optics maintenance kits, and operator training packages globally.
Direct technical answers from application engineers to streamline equipment evaluation.
