Explore our premium lineup of industrial laser systems engineered for high precision, zero-deformation surface hardening, metal welding, cladding, and multi-functional metal fabrication.








In modern heavy machinery, automotive manufacturing, aerospace engineering, and precision tooling, surface wear and localized mechanical stress represent over 75% of premature component failures. Traditional surface hardening techniques—such as flame hardening, induction heat treating, gas nitriding, and carburizing—frequently introduce critical bottlenecks into high-throughput production lines. These traditional methods inherently suffer from massive thermal distortion, inconsistent case depth, requirement for chemical/liquid quenching media, and intensive post-process grinding operations.
As premier China Laser Hardening Manufacturers & Exporters, we specialize in high-power Direct Diode Laser Hardening (DDLH) and Fiber-Delivered Laser Surface Engineering systems. By focusing coherent laser energy into customizable rectangular or scanning beam profiles, our advanced laser hardening equipment delivers localized, highly precise surface austenitization. With thermal heating rates exceeding thousands of degrees per second followed by rapid self-quenching via conduction into the cold bulk material, laser hardening achieves superior fine-grained martensitic microstructures with virtually zero geometric distortion.
Direct from our state-of-the-art applications laboratory, these key engineering breakthroughs define the next generation of industrial surface processing equipment exported worldwide.
Thermal stability is the single most critical factor in achieving repeatable case depth without surface melting. Our laser hardening heads integrate coaxial infrared pyrometers operating at PID sampling frequencies up to 1000 Hz. The system dynamically modulates laser output power in real time to compensate for changing component mass, geometry, and thermal heat sinks.
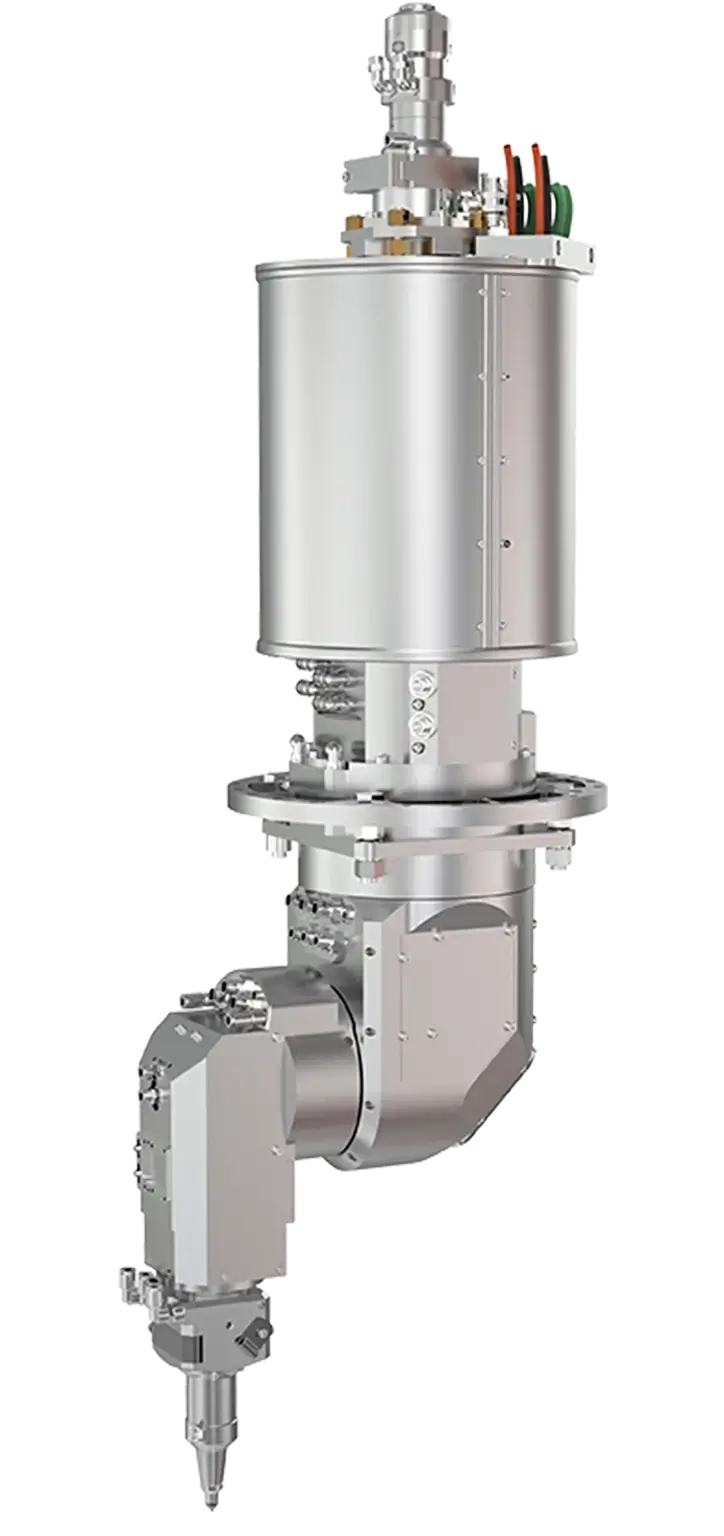
Unlike Gaussian laser beams that create hot spots and inconsistent hardness gradients, our specialized laser heads utilize multi-faceted optical beam integrators or high-frequency 2D galvo scanning optics. This homogenizes the beam into uniform rectangular profiles (ranging from 10x10mm up to 60x12mm), guaranteeing flat-top power distribution across complex geometries.
Complex 3D workpieces—such as automotive stamping dies, turbine blade roots, transmission gear shafts, and heavy-duty crane wheels—require flexible multi-axis positioning. We integrate high-precision 6-axis industrial robots synchronized with 2-axis positioners to execute continuous, complex spatial laser hardening paths with sub-millimeter accuracy.
Technical Insight: Laser hardening utilizes the substrate's own mass for conductive cooling (self-quenching). Heating rates exceed 1000°C/sec with cooling rates reaching 500°C/sec. This self-quenching mechanism yields a homogeneous, ultra-fine homogeneous martensite structure, often exceeding conventional quench-and-temper hardness by 2 to 5 HRC points!
Comparing high-power Direct Diode Laser Hardening against traditional industrial surface heat treatment processes:
| Process Parameter | Direct Diode Laser Hardening | Induction Hardening | Flame Hardening | Gas Nitriding / Carburizing |
|---|---|---|---|---|
| Heat Affected Zone (HAZ) | Extremely Micro-Localized | Moderate to Large | Very Large & Uncontrolled | Entire Component Exposed |
| Post-Process Distortion | Near Zero (< 0.05 mm) | Significant (Requires Grinding) | Severe Distortion / Warpage | Low to Moderate Warpage |
| Quenching Medium Required | None (Self-Quenching) | Water, Polymer, or Oil | Water Spray / Immersion | Gas / Liquid Coolant |
| Process Energy Efficiency | High (Direct Energy Coupling) | Moderate | Low (Fossil Fuel Waste) | Low (Long Furnace Hours) |
| Closed-Loop Thermal Control | Yes (Real-time Pyrometer) | Rare / Complex | No (Manual Observation) | Atmospheric PID Only |
Procurement directors and plant operational leaders must adapt to evolving global manufacturing trends. Below are the key directional forces shaping international procurement of laser surface processing machinery.
Global environmental regulations, carbon border taxes, and strict ESG compliance standards are forcing manufacturing hubs to eliminate toxic chemical quenches, oil baths, and energy-intensive furnace operations. Industrial laser hardening operates completely dry without polymer or oil quenches, reducing carbon footprints by up to 60% compared to gas carburizing furnaces.
Future laser hardening machinery procurement will heavily prioritize Industry 4.0 integration. Overseas buyers are demanding full OPC-UA and MES telemetry connectivity. Modern Chinese exporters now supply integrated machine-vision systems and AI models that detect micro-melting in real time, auto-correcting robot feed speed and power to guarantee zero scrap rates during high-value die hardening.
Multi-process capability is replacing single-function machines. Leading exporters now design dual-purpose laser cells capable of switching between laser surface hardening (heat treatment) and ultra-high-speed laser cladding (EHLA) (corrosion & wear coating deposition). This drastically lowers total capital expenditure (CAPEX) for global rebuilding and remanufacturing facilities.

As a established OEM manufacturer and global exporter, our engineering strength ensures seamless machine integration, technical compliance, and long-term operating reliability.
All machine enclosures are constructed strictly under Class 1 laser safety protocols with fail-safe safety interlocks, optical density (OD6+) certified viewing windows, and built-in industrial fume extraction integration.
We do not just sell standard equipment; we validate your metallurgy. Our dedicated R&D lab provides full sample trial reports, hardness depth profiling (Vickers micro-hardness), optical metallography, and cycle-time studies prior to machine order finalizing.
From pre-shipment Factory Acceptance Testing (FAT) to overseas Site Acceptance Testing (SAT), operational training, maintenance spare kits, and 24/7 remote optical/PLC diagnostic support, our global export network supports installations in over 40 countries.
A laser machine's long-term accuracy depends heavily on structural stability. All our custom multi-axis laser hardening systems utilize stress-relieved welded steel frames or natural granite beds to eliminate vibration, ensuring sub-micron motion repeatability during continuous 24/7 industrial production runs.
Whether you require standard 4-in-1 portable fiber laser devices or custom multi-kilowatt robotic laser hardening cells, our engineering team tailors optics, laser wavelength, and motion kinematics to your exact factory specifications.
Comprehensive answers to critical technical questions asked by international procurement directors, metallurgists, and plant managers.
Laser hardening is effective on all medium-to-high carbon steels (carbon content ≥ 0.35%), alloy steels, tool steels, and ductile/grey cast irons. Typical compatible grades include AISI 4140/42CrMo4, C45, 1045, D2, H13, and GGG60 cast iron. Standard case depths range from 0.5 mm up to 2.5 mm per pass depending on laser power, travel speed, and material hardenability, delivering surface hardness ratings between 55 and 65 HRC.
Unlike induction or furnace heating which raises the temperature of the entire part or a large volume of metal, laser hardening deposits concentrated energy extremely fast into only the top surface layer (austenitization). Because the surrounding cold bulk material acts as an instantaneous heat sink (self-quenching), thermal expansion is localized and restrained, keeping overall component geometric distortion below 0.02 mm–0.05 mm and eliminating expensive post-hardening finish grinding.
Direct Diode Lasers (DDL) emit wavelengths around 900 nm – 1020 nm, which exhibit significantly higher absorption efficiency on raw steel surfaces (up to 40-50% absorption) compared to Fiber (1064 nm) or CO2 (10.6 µm) lasers. Furthermore, Direct Diode laser sources natively produce rectangular or line beam geometries ideal for uniform track hardening, operating at wall-plug electrical efficiencies exceeding 45%.
Standard machines have lead times of 30 to 45 days, while custom robotic special-purpose machines (SPM) typically require 60 to 90 days. Every export shipment includes full CE compliance certificates, optical safety test reports, complete electrical/pneumatic schematics, user operation manuals, and spare component kits. We dispatch senior application engineers for overseas installation, SAT, and operator training, backed by 24/7 remote optical diagnostic support.
Yes. By utilizing modular optical quick-change interfaces, our multi-functional laser systems can swap between a pyrometer-integrated laser hardening head (wide homogenized beam) and a high-speed laser cladding/welding head (coaxial powder/wire feed optics). This flexible setup is widely adopted by international remanufacturing and contract job shops.
When hardening adjacent tracks or complex geometric corners, heat accumulation can cause surface overheating or melting. Our high-speed infrared pyrometer measures surface temperature at 1000 Hz directly in the laser spot. The closed-loop controller instantly drops the laser power output when the surface reaches the target austenitizing temperature (e.g., 1050°C), maintaining perfectly uniform hardness without surface degradation.
Contact our sales engineering team today for technical consultations, customized machine quotes, or sample processing testing for your production line.
