Explore our ISO-certified industrial laser platforms built for high-throughput sheet metal processing, tube cutting, and custom fabrication.
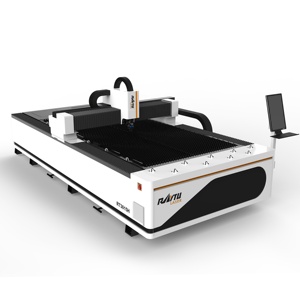
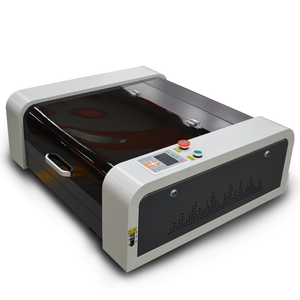
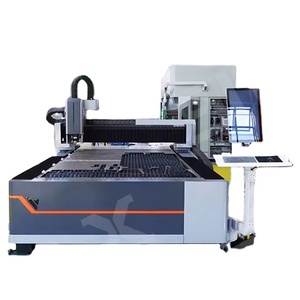
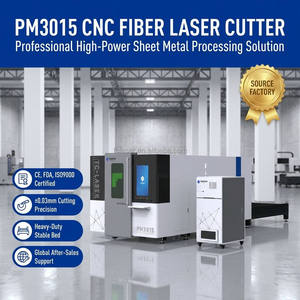
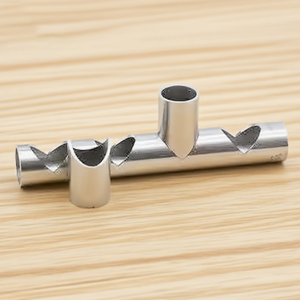
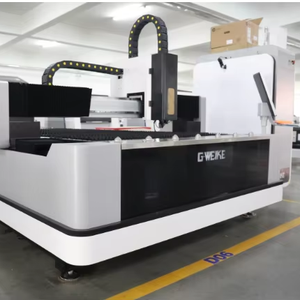
Combining over three decades of optical research, rigorous ISO-certified manufacturing processes, and localized international support networks.
We manufacture optical components, motion control algorithms, and heavy-duty machine frames under one roof. Our state-of-the-art applications lab tests every cut profile prior to shipment.
Engineered to international safety standard CE Class 1. Integrated with multi-zone environmental partition smoke filtration, preventing particulate emissions during continuous production shifts.
Direct factory technicians perform site acceptance testing (SAT), operator training, and preventative maintenance worldwide, reinforced by cloud-based remote diagnostic IoT telemetry.
In the modern global manufacturing landscape, precision metal processing has evolved from conventional mechanical stamping and plasma torch cutting toward ultra-high-efficiency fiber laser beam machining. As China solidifies its position as the world leader in optoelectronic equipment manufacturing, selecting the right metal laser manufacturer and factory requires an in-depth technical evaluation of laser physics, beam delivery systems, structural gantry mechanics, and total cost of ownership (TCO). This comprehensive industrial whitepaper provides global procurement managers, factory directors, and OEM engineering teams with the domain knowledge necessary to benchmark fiber laser cutting systems, evaluate supplier capabilities, and navigate emerging laser material processing trends for 2025–2030.
Key Technical Insight: Wall-plug efficiency for solid-state fiber lasers now exceeds 40%, drastically reducing operational electrical costs compared to legacy CO2 systems (which operate at 8–10% efficiency). Selecting a machine with high-fidelity beam beam parameters ($M^2 < 1.2$) ensures minimal kerf width and zero burr formation on complex metallurgical alloys.
A high-performance industrial CNC fiber laser cutting machine is an integrated system combining light emission optics, motion mechanics, gas dynamics, and computerized numerical control. Understanding the key sub-assemblies is critical when auditing a China laser factory:
The laser source generates photon energy through Ytterbium-doped optical fiber modules pumped by semiconductor diodes. The output wavelength of ~1064 nm is readily absorbed by ferrous and non-ferrous metals alike, including carbon steel, stainless steel, aluminum, brass, and copper. Key optical parameters include:
Laser power is ineffective without a rigid, vibration-damped mechanical foundation. Premium Chinese metal laser manufacturers utilize structural machine beds made of heavy welded steel plates or high-density cast iron that undergo high-temperature thermal annealing (stress relieving at 600°C for 24 hours) to eliminate internal stress.
The cross-gantry is increasingly engineered from extruded aviation-grade aluminum alloy, created via a 10,000-ton hydraulic press process. This minimizes moving mass, enabling accelerations of up to 1.5G to 2.5G without sacrificing positional accuracy along the X/Y linear guide rails.
| Technical Parameter | Standard Entry-Level System | Heavy Industrial CNC Fiber Cutter | High-Precision 5-Axis System |
|---|---|---|---|
| Laser Power Range | 1,000W – 2,000W | 3,000W – 30,000W (30KW) | 4,000W – 12,000W |
| Positioning Accuracy | ±0.05 mm/m | ±0.03 mm/m | ±0.015 mm/m |
| Max Acceleration | 0.8G – 1.0G | 1.5G – 2.0G | 2.5G+ |
| Cutting Gas Options | Oxygen (O2), Air | High-Pressure Nitrogen (N2), Air, O2 | Clean Compressed Air, N2 |
| Machine Bed Treatment | Standard Welded Frame | Stress-Relieved Mortise & Tenon Steel | Granite Base / Cast Iron Bed |
As global supply chains demand higher throughput, lower carbon footprints, and greater manufacturing agility, industrial laser procurement strategies are shifting dramatically. Buyers seeking suppliers in China should evaluate factories aligned with the following technological trends:
The industry has crossed the threshold where 20KW, 30KW, and even 60KW fiber lasers are replacing traditional mechanical sawing, plasma cutting, and oxy-fuel cutting for thick carbon steel plates up to 100mm. The primary driver is economic: ultra-high power lasers permit high-pressure compressed air cutting instead of expensive liquid nitrogen (N2) or oxygen (O2), lowering gas processing costs by up to 80% while maintaining clean, oxide-free edges.
Environmental standards such as Euro 7 and international ESG compliance mandate strict particulate matter collection inside sheet metal processing plants. Next-generation metal laser machinery incorporates zone-partitioned dust extraction systems. Smoke exhaust dampers automatically open only directly beneath the active cutting head, reducing suction power requirements by 50% while channeling 99.97% of metal fumes through multi-stage HEPA and activated carbon filtration units.
Traditional 2D flatbed sheet cutting is being complemented by dynamic 5-axis laser cutting heads capable of trimming hydroformed metal components, curved automotive structural pillars, and complex stamped tube profiles in a single pass. Paired with 6-axis articulated industrial robots and automated material loader/unloader tower systems, modern laser factories run unassisted "lights-out" manufacturing shifts around the clock.
Leading manufacturers now equip cutting heads with embedded infrared pyrometers and acoustic sensors that monitor cut quality in real-time. If plasma blowout, thermal runaway, or nozzle contamination is detected, the CNC controller automatically adjusts laser power frequency, feed rate, and assist gas pressure dynamically, virtually eliminating scrapped workpieces.
When evaluating quotations from a China metal laser factory, looking solely at the upfront equipment purchase price ($CAPEX$) leads to inaccurate financial forecasting. Procurement teams must model operational expenditure ($OPEX$) over a 5-year equipment lifecycle using the following cost matrix formula:
Total Cost of Ownership Formula:
$$TCO = CAPEX + \sum_{t=1}^{5} \left( E_{electrical} + G_{assist\_gas} + M_{maintenance} + C_{consumables} - R_{residual\_value} \right)$$
Gas consumption represents the largest ongoing variable expense in fiber laser operation:
Standard consumables include protective quartz cover glasses, copper nozzles, and ceramic sensor rings. Premium factories utilize capacitive height-tracking heads with sealed protective windows that shield interior optics from metal spatter, extending component lifespan from 100 operating hours to over 500 hours per optical element.
To ensure high operational reliability, overseas buyers should verify that prospective OEM factory suppliers in China fulfill the following structural and quality assurance protocols:
Before dispatch, every precision CNC laser bed must be calibrated using a Renishaw multi-axis laser interferometer. This measures linear positioning errors, pitch, yaw, and repeatability across the entire travel distance, ensuring compliance with ISO 230-2 accuracy standards.
A circularity test using a wireless telescoping ballbar validates gantry squareness and servo tuning at dynamic feed rates. Deviations from a true circular trajectory highlight backlash in the helical gear racks or mismatch in X/Y drive motor responsiveness.
Industrial fiber lasers operate at Class 4 invisible laser levels (1064nm). Factory enclosures must feature certified protective observation windows (OD6+ optical density) and dual-circuit safety interlocks that terminate laser emission immediately if enclosure doors are opened during cycle execution.
Expert technical responses to critical procurement, installation, and engineering queries.
Selection depends on your primary material thickness distribution and target production speed. A 3KW system efficiently cuts carbon steel up to 20mm and stainless steel up to 8mm. A 6KW laser doubles processing speed on 6-10mm metals and increases maximum carbon steel capacity to 25mm. A 12KW platform is optimized for high-speed compressed air cutting on mid-to-thick plates (12mm to 40mm) where maximum throughput and minimum unit cost are paramount.
The facility requires a level reinforced concrete floor (minimum 200mm thickness to prevent vibration propagation), a 3-phase electrical supply (380V/480V depending on region) with dedicated voltage stabilization, clean industrial compressed air piping (if using air cutting), and adequate clearance for loading raw sheet stock via overhead crane or forklift automation.
Standard CNC flatbed laser cutters are built and undergo Factory Acceptance Testing (FAT) within 20 to 30 days. Custom automated lines or enclosed multi-axis systems take 45 days. Every delivery includes comprehensive operation manuals, wiring diagrams, and optional direct dispatch of factory service engineers for Site Acceptance Testing (SAT), alignment verification, and operator training.
Unlike legacy open exhaust channels that lose suction across large beds, partitioned extraction opens heavy pneumatic valves only underneath the specific bed zone where the laser head is actively processing metal. This concentrates vacuum pressure, capturing dangerous sub-micron metal particles, zinc fumes from galvanized steel, and oil residue before it can disperse into the shop floor environment.
Send us your part drawings, material specifications, and production volume targets. Our senior applications team will provide a comprehensive laser selection analysis and sample cutting report within 24 hours.
